7 Tips for Choosing Indexable Milling Tools?

Choosing the right Indexable Milling tool affects cycle time, surface quality, insert life, and production stability. The decision is rarely as simple as selecting the largest cutter or the highest cutting speed. Material grade, machine power, workholding rigidity, and chip evacuation all influence the result. A cutter that performs well in hardened steel may struggle in aluminum.

Industry data supports this careful approach. The U.S. Manufacturing Technology Orders report, published by AMT, tracks continuing investment in advanced machining equipment and automation. These investments increase pressure to reduce idle time and improve process consistency. Deloitte’s 2024 Global Manufacturing Industry Outlook also highlights productivity, labor shortages, and digital manufacturing as major industry concerns. Better tooling choices can address each issue, but only when cutting data matches real shop conditions.

This guide presents seven practical tips for evaluating Indexable Milling tools. It examines insert geometry, substrate grade, cutter diameter, lead angle, coating, coolant strategy, and toolpath behavior. ISO 8688 provides recognized methods for evaluating milling tool life, yet laboratory results do not always represent a vibrating machine or interrupted cut. That limitation matters. A tool may last for hours in a controlled test, then fail after several unstable passes on the shop floor.

Experienced machinists usually begin with the workpiece and machine, not the catalog photograph. They check spindle torque, holder runout, fixture support, and chip thickness. Small details matter. A loose fixture can destroy an expensive insert quickly. The following recommendations combine manufacturer guidance, machining practice, and measurable production factors to support safer, more reliable decisions.

7 Tips for Choosing Indexable Milling Tools?

Understanding Indexable Milling Tool Basics and Applications

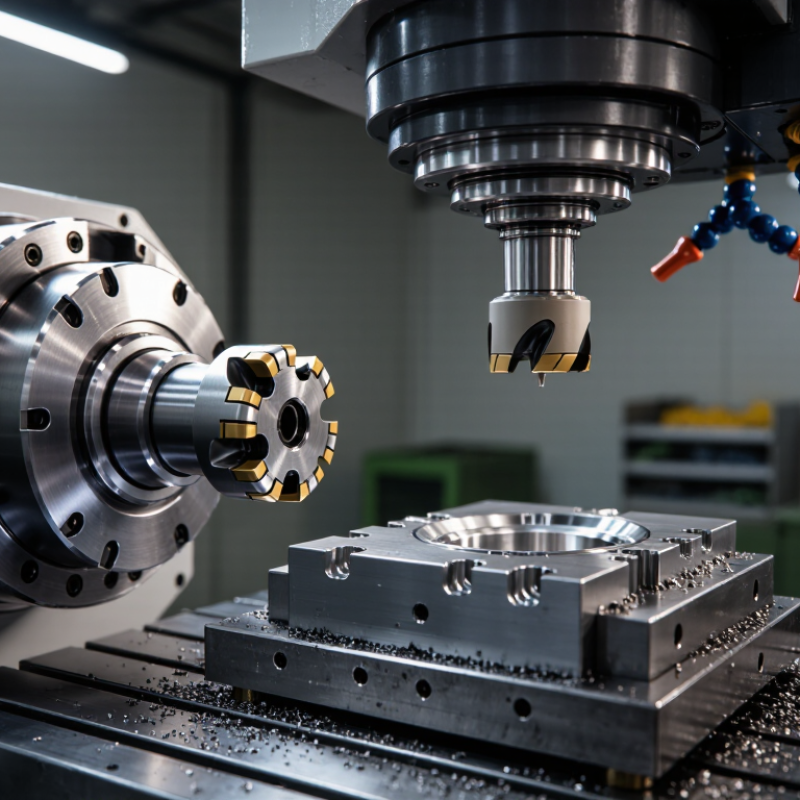
Choosing an indexable milling tool starts with understanding its basic construction. The cutter body holds replaceable inserts, while each insert provides a cutting edge. When one edge wears, the insert can be rotated or replaced. This reduces downtime, but only when the insert seats cleanly. Check the pocket for chips before tightening it. A thin chip trapped underneath can create runout and uneven cutting.

Match the insert geometry to the material and operation. A sharp edge suits aluminum and other softer materials, while a stronger edge handles interrupted cuts in steel. Select the cutter diameter according to the machine’s power and the required step-over. Larger is not always better. Confirm the insert grade, rake angle, and cutting direction from reliable technical data. Then set speed, feed, and depth of cut within proven limits. Watch the chips. Powdery chips may indicate rubbing, while long, hot chips can signal poor evacuation.

Application conditions matter as much as tool selection. A rigid setup supports heavy roughing, but a slender workpiece may need lighter radial engagement. Use coolant only when the insert and material allow it; thermal shock can damage some cutting edges. During production, listen for chatter and inspect the insert corners after a short trial pass. I have sometimes blamed the tool when the real problem was weak workholding. That mistake is easy to repeat. Record successful settings beside the machine, including material, insert condition, and measured tool life. Small records often improve the next job more than aggressive cutting changes.

Matching Tool Geometry to the Workpiece Material

Choosing an indexable milling tool starts with the workpiece, not the insert catalog. Aluminum usually needs a sharp, positive-rake edge and polished flutes. These features reduce built-up edge and help chips leave the cut quickly. Cast iron behaves differently. A stronger edge and a negative or neutral rake can resist abrasive particles and interrupted cutting. Stainless steel needs careful heat control because it work-hardens under rubbing. Use a sharp edge, stable clamping, and enough feed per tooth.

Tip 1: Match geometry to the material’s hardness, ductility, and chip behavior. The wrong rake angle can turn a quiet cut into vibration, heat, and premature edge failure. The U.S. Cutting Tool Institute and AMT reported approximately 2.60 billion dollars in U.S. cutting-tool consumption during 2023. That figure fell 6.2% from 2022, making tool-life decisions more important for many shops. Data does not replace a cutting test, though.

Tip 2: Check the insert grade and chipbreaker together. A tough grade may survive interrupted cast-iron cuts, while a wear-resistant grade can suit continuous steel machining. Tip 3: Watch the first chips. Blue chips, welded material, or a bright rubbing line suggest poor geometry or insufficient feed. In my experience, machinists often blame speed too quickly. I have made that mistake. A rigid setup can reveal that the real problem is an overly weak edge or an unsuitable chipbreaker. Record tool life, cutting sound, and surface finish after each trial. Small records prevent expensive guesses.

7 Tips for Choosing Indexable Milling Tools? - Matching Tool Geometry to the Workpiece Material

Tip Workpiece Material Recommended Tool Geometry Insert Grade and Coating Cutting-Edge Design Starting Cutting Parameters Key Selection Reason
1 Low-carbon steel
Typical hardness: below 200 HB
Positive or moderately positive rake; medium tooth pitch; standard helix for general-purpose milling. Tough carbide substrate with a wear-resistant multilayer coating suitable for steel machining. Sharp edge with a small hone to balance cutting ease and edge strength. Cutting speed: 120–220 m/min
Feed per tooth: 0.08–0.20 mm/tooth
Positive geometry reduces cutting forces and helps prevent built-up edge in ductile steel.
2 Stainless steel
Austenitic grades may work-harden
High-positive rake, variable helix, and unequal pitch to reduce vibration and maintain a free-cutting action. Tough, heat-resistant carbide with a smooth coating that limits adhesion and crater wear. Very sharp edge with a controlled hone; avoid excessive edge rounding. Cutting speed: 60–140 m/min
Feed per tooth: 0.05–0.15 mm/tooth
A sharp, stable edge limits heat generation and reduces the risk of work hardening.
3 Cast iron
Gray and ductile iron
Neutral to slightly positive rake; rigid body; medium or coarse pitch for chip clearance and interrupted cuts. Wear-resistant carbide grade with a coating designed for abrasive dust and thermal cycling. Reinforced edge preparation and a secure insert seat to withstand interrupted engagement. Cutting speed: 100–250 m/min
Feed per tooth: 0.10–0.25 mm/tooth
A stronger edge resists abrasion, chipping, and thermal shock from intermittent cutting.
4 Aluminum alloys
Especially soft, ductile grades
Strongly positive rake, high helix, and wide chip gullets; use fewer teeth when chip volume is high. Fine-grain carbide with a polished, low-adhesion surface; uncoated or non-reactive coatings are commonly suitable. Highly polished, sharp edge with minimal edge hone to produce a clean surface. Cutting speed: 300–800 m/min
Feed per tooth: 0.08–0.30 mm/tooth
Large gullets evacuate bulky chips and a polished edge helps prevent material buildup.
5 Titanium alloys
Low thermal conductivity
Positive rake, variable pitch, and a stable body; prefer a geometry that supports shallow radial engagement. Tough carbide with a heat-resistant coating and strong resistance to edge chipping. Sharp but reinforced edge; avoid rubbing by maintaining sufficient feed per tooth. Cutting speed: 30–80 m/min
Feed per tooth: 0.04–0.12 mm/tooth
Low speed and positive geometry help control heat, while variable pitch reduces chatter.
6 Hardened steel
Approximately 45–60 HRC
Rigid, low-positive or neutral geometry; variable pitch and a short tool overhang are preferred. Fine-grain carbide for moderate hardness; advanced hard-material grades may be considered above the carbide range. Precisely honed edge with strong support; inspect frequently for micro-chipping. Cutting speed: 40–100 m/min
Feed per tooth: 0.03–0.10 mm/tooth
A rigid, wear-resistant system withstands high cutting pressure without sacrificing dimensional control.
7 Heat-resistant nickel alloys
High-temperature aerospace alloys
Positive cutting action, variable pitch, and a geometry designed for low radial engagement and efficient coolant delivery. Tough, heat-resistant carbide with a stable coating; use a grade intended for difficult-to-cut alloys. Sharp, heavily supported edge with a controlled hone; replace inserts at the first sign of notch wear. Cutting speed: 20–60 m/min
Feed per tooth: 0.03–0.10 mm/tooth
Low thermal conductivity and work hardening demand controlled heat, consistent engagement, and strong edge support.
Important: Cutting parameters are starting ranges for carbide indexable milling tools. Final values should be adjusted according to insert size, cutter diameter, machine rigidity, workholding, coolant strategy, radial and axial engagement, and the actual workpiece condition.

Choosing Inserts for Cutting Performance and Surface Quality

7 Tips for Choosing Indexable Milling Tools
Choosing Inserts for Cutting Performance and Surface Quality

Selecting an insert is not only a matter of matching its grade to the workpiece. The cutting edge must suit the material, machine rigidity, and milling direction. For hardened steel, a tougher edge may resist chipping. Aluminum often needs a sharper, highly polished cutting edge to prevent built-up material. Watch the chips closely. Long, stringy chips can signal poor geometry or incorrect cutting data.

Surface quality depends on more than insert grade. A positive rake angle can reduce cutting force, while a stable, finely honed edge may improve tool life. Choose the corner radius carefully. A larger radius can support heavier cuts, but it may increase vibration on a thin component. Check insert runout after installation. Even a small height difference can leave visible lines across the machined face.

Keep the holder clean and tighten each insert consistently. Coolant placement also matters, especially when heat gathers near the cutting zone. I once blamed the insert for a rough finish, but the real problem was excessive tool overhang. That assumption was wrong. Test one variable at a time, record feed, speed, depth of cut, and insert wear. Do not rely on appearance alone. Measure roughness when the surface specification is important. Small edge damage may remain hidden until several parts have been machined.

7 Tips for Choosing Indexable Milling Tools

Choose insert geometry, grade, nose radius, and edge preparation according to the workpiece material, cutting conditions, and required surface quality. A larger nose radius can improve surface finish, but it also increases cutting forces and may cause vibration in less rigid setups.

  1. Match the insert grade to the workpiece material and cutting temperature.
  2. Select a positive geometry for lower cutting forces and improved machinability.
  3. Use a stronger negative geometry for heavy roughing and interrupted cuts.
  4. Choose a nose radius that balances surface finish, rigidity, and cutting force.
  5. Use a chipbreaker designed for the actual feed and depth-of-cut range.
  6. Apply a sharp edge for aluminum and other ductile materials; use a reinforced edge for hard or interrupted cuts.
  7. Verify tool overhang, coolant delivery, and machine rigidity before increasing cutting parameters.

The chart shows theoretical arithmetic surface roughness, Ra, calculated from Ra ≈ f²/(32rε), where f is feed per revolution and rε is insert nose radius. Actual results vary with workpiece material, tool condition, machine rigidity, vibration, and cutting parameters.

Evaluating Tool Size, Holders, and Machine Compatibility

Choosing an indexable milling tool starts with the machine, not the catalog. Measure spindle taper, available torque, maximum speed, and the machine’s working envelope. A cutter that fits the spindle may still strike the enclosure. Tool diameter also matters. Large bodies improve productivity, but they increase cutting force and may overload a smaller spindle. Check the machine manual, then verify the real clearance with the holder installed.

Holder selection deserves equal attention. Match the holder to the spindle interface and cutter connection, such as a shell-mill arbor or modular system. Keep gauge length short. Long setups amplify vibration and reduce surface quality. I measure runout near the inserts, preferably below 0.01 mm for demanding finishing work. That target is practical, but not universal. Roughing, thin walls, and unstable workpieces may need different priorities. Cooling passages, pull-stud condition, and clamping force should also be inspected.

Machine compatibility increasingly affects automated production. The International Federation of Robotics reported 4,281,585 industrial robots operating worldwide in 2023. That scale makes repeatable tool length and holder seating more important. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of manufacturers view smart manufacturing as important for competitiveness. However, digital monitoring cannot correct a poorly sized cutter. Test one toolpath first. Check spindle load, vibration, chip shape, and insert wear. I have seen excellent cutting data fail because the holder was simply too long. Rechecking assumptions is worthwhile.

Balancing Cost, Tool Life, and Maintenance Requirements

7 Tips for Choosing Indexable Milling Tools

Choosing indexable milling tools is not just a price comparison. In the shop, a cheaper cutter can become expensive after repeated insert changes, setup delays, and poor surface quality. Tip one: calculate cost per finished component, not cost per tool. Include inserts, labor, downtime, and scrap. Tip two: match the tool body to the machine’s rigidity and spindle power. A heavy cutter may look productive but perform poorly on a light machine. Tip three: select insert geometry for the material and cutting depth. The wrong geometry shortens tool life quickly.

Small details matter. Tip four: compare expected tool life under realistic cutting conditions. Supplier charts help, but actual results depend on coolant, workholding, and operator habits. Keep records. Tip five: choose a system with practical insert access. If changing an insert requires removing guards or fixtures, maintenance costs rise. Tip six: inspect screw seats, pockets, and cutting edges during every change. A small chip can damage the tool body and create unstable cutting.

Do not chase maximum life blindly. A very long-lasting insert may require slower feeds, reducing productivity. Tip seven: balance tool life against cycle time and replacement frequency. I have seen teams overlook cleaning because the tool still “looks usable.” That judgment can be costly. Clean pockets, use the correct torque, and check runout regularly. Even experienced machinists occasionally overestimate a tool’s remaining life, so measured wear is safer than intuition.